When we’re talking about a front assembly riveting production line, the inspection method we use can’t just be “quick glance and call it good”—that’s how you end up with a faulty part on the assembly line that causes a whole lot of rework, or even worse, a product that leaves your facility with hidden issues. As a supplier who’s worked on these lines for over 12 years, I’ve seen every mistake: a missed rivet shank, a formed head that’s too weak, a misaligned joint that’ll work its loose six months down the line. Our riveting line’s inspection process isn’t a single step—it’s a layered, real-time thing that ties directly into every machine on the line, not something we tack on at the end after all the rivets are set. Let me break down how this works, like I’d walk a new client through it at our tech lab on a Tuesday morning. Front Assembly Riveting Production Line
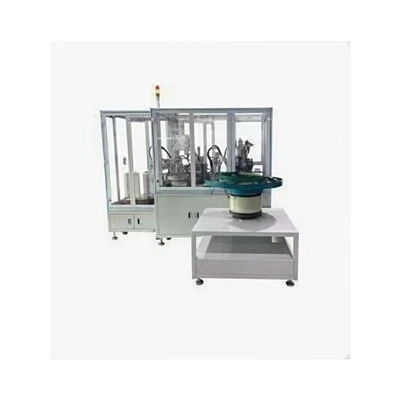
First off, we don’t rely on humans to catch every single defect during the active riveting step. Wait, hear me out—manual checks are still super important, but they’re for the final “quality gate,” not for the split second after a rivet is set. The first layer is what we call in-process closed-loop inspection, and it’s baked right into each rivet station on the line. Each riveting gun is hooked up to a controller that tracks three metrics, live, as the rivet gets squeezed into the workpiece. The first is force displacement: when the gun fires, it doesn’t just push a set amount of force—we measure how the rivet deforms as force is applied. If it’s a solid rivet, a good one will have a smooth, predictable displacement curve; if there’s a hidden void in the rivet shank or the joint gap is too big, that curve will spike or dip, and the machine will stop mid-cycle. That’s not a hard stop that throws away a good part—we program it to pause and log the exact reading so an operator can confirm if it’s a glitch (like a dirty rivet) or a bad component. The second metric is head diameter and height. We use a small, non-contact laser sensor right above the rivet head, mounted on the same tooling as the gun. Right after the rivet is formed, it snaps a 3D image of the head, compares it to a pre-approved part profile, and rejects it on the spot if it’s too small (meaning not enough force) or too lopsided (meaning the gun was misaligned). No moving the part off the line, no waiting for a separate quality team to check—every rivet gets a pass/fail before the next part even hits the station.
Then there’s the gap inspection step, which is the one most riveting lines skip, but it’s the number one cause of joint failure. A lot of people think “rivet tight” means the joint’s tight, but if two panels are 0.2mm apart where a rivet goes, that rivet will set but won’t distribute load evenly, and over time, the panels will separate. We integrated a pair of eddy current sensors into the workholding fixture after every 10 rivet stations. These run a quick scan across the entire surface of the front assembly (that’s the thing we’re riveting—usually a car door inner, a appliance front panel, or a aerospace component, depending on the line) and measure the distance between every pair of joined surfaces. If a gap is larger than our tolerance (we set that per client, usually 0.15mm for automotive), the sensor flags it, and the part moves to a station where an automated clamp adjusts the gap before any more rivets are added. This stops a part that’s got a hidden gap from moving forward, which saves tons of time because you don’t have to drill out and re-rivet later. I’ve had clients tell me they cut their rework rate on front assembly lines by 80% after we added these sensors—they didn’t even know gap inspection was the missing piece until we showed them.
Now, after all the in-process checks, we have a final automated quality gate that’s a mix of visual verification and non-destructive testing (NDT) that’s specific to rivets. A lot of lines use basic camera systems that just check for a “head is there,” but we use a high-resolution RGB camera with edge detection software that catches tiny defects: a micro-crack in the rivet head that’s only 0.1mm wide, a slight burr that’s sharp enough to cut wiring later, or a rivet that’s misaligned by a fraction of a degree. The camera also cross-references the part’s serial number (we add a QR code to the front assembly early in the line) with our quality database, so if a rivet fails, we can pull up exactly which station it was set in, what the force displacement was, and even which rivet batch came from. That’s huge for root cause analysis—if a whole batch of rivets is bad, we catch it before it ruins a run of parts.
But here’s the thing: even with all that tech, manual checks are still non-negotiable. We schedule a 100% manual visual and tactile inspection of every part that passes the automated gates, but it’s not just “look at it.” Our operators go through a quick checklist: run a fingernail along the rivet heads to catch any sharp burrs (machines don’t always pick those up), check that no rivets are missing in the pattern (we had one client where a camera missed a tiny 2mm rivet, but a human caught it right away), and tap each rivet with a small metal hammer to listen for a hollow sound. A hollow thud means the rivet is not fully set, which a laser might miss if the head is the right size but the shank is incomplete. We train our operators to do this in 90 seconds per part, so it doesn’t slow down the line at all—we built the quality gates to work with their workflow, not against it.
We also do periodic destructive testing, but it’s not for every part. Every 500 parts (or per client request, more often if they’re running high-stakes components like medical device parts), we pull a sample, cut it open, and check the rivet’s shear strength and the bond between the rivet and the workpiece. We log all those results in the same database as the in-process metrics, so clients can see a full audit trail of every rivet that left the line. A lot of our competitors say “destructive testing is optional,” but we think it’s necessary to confirm the automated systems are calibrated right—if a sensor is out of alignment, destructive testing will catch that before it leads to a recall.
Wait, let me make this concrete with an example. Last quarter, we set up a front assembly line for a major appliance brand that was having issues with door panels coming loose during shipping. They were using a standard riveting line with only a final visual check, and about 3% of their parts were failing after assembly. We added the closed-loop force sensors, the eddy current gap scanners, and the manual tactile check, and their failure rate dropped to 0.1% within the first month. They didn’t change the rivets or the guns—they just added the inspection steps that tie directly to the riveting process, not after. That’s the big difference between a “riveting line” and a “riveting line with robust quality.”
I know a lot of clients come to us thinking inspection is something you bolt onto the end of the line, but it’s not. It’s integrated into every step, so you don’t waste time and material on parts that are going to fail later. We also offer full calibration for all the sensors, and yearly training for operators so they know how to spot rare defects the machines might miss. If you’re setting up a new front assembly riveting line, or upgrading an old one, the key is that your inspection method has to work with the riveting process, not against it. You don’t want a machine stopping for a tiny glitch every other part, but you also don’t want to send a bad part out because you skipped a step.

At the end of the day, the riveting quality method on our lines is built to give our clients peace of mind: every rivet is checked in real time, gaps are scanned before they cause issues, and a human double-checks the stuff tech can’t always catch. If you’re looking to set up a front assembly riveting line, or upgrade your current one, we can walk you through exactly how this works for your specific part needs. Reach out to our team to chat through your quality goals, and we’ll show you how our inspection process cuts your rework, reduces failure rates, and keeps your line running smoothly.
Enclosed Integrated Lead Screw Linear Module References
- ASME Standard B111M-2018: Specification for Riveting Machines and Equipment
- ISO 10846-2:2019: Non-Destructive Testing of Riveted Joints – Eddy Current Testing Methods
- Automotive Industry Action Group (AIAG) Core Tools: Advanced Product Quality Planning (APQP) for Riveting Processes
Yangning (Xiamen) Intelligent Technology Co., Ltd.
With abundant experience, we are one of the most professional front assembly riveting production line manufacturers in China. As we have world-leading production equipment and strong manufacturing capabilities, we warmly welcome you to buy bulk advanced front assembly riveting production line from our factory. Customized orders are welcome.
Address: Room 307-2, No. 15 Duiying Road, Software Park Phase III, Torch Hi-Tech Zone, Xiamen, Fujian, China
E-mail: mia@ynautos.com
WebSite: https://www.ynautos.com/
